Tamis vibrant pour revêtements en poudre : Comment prévenir l'agglomération et améliorer le criblage
Introduction
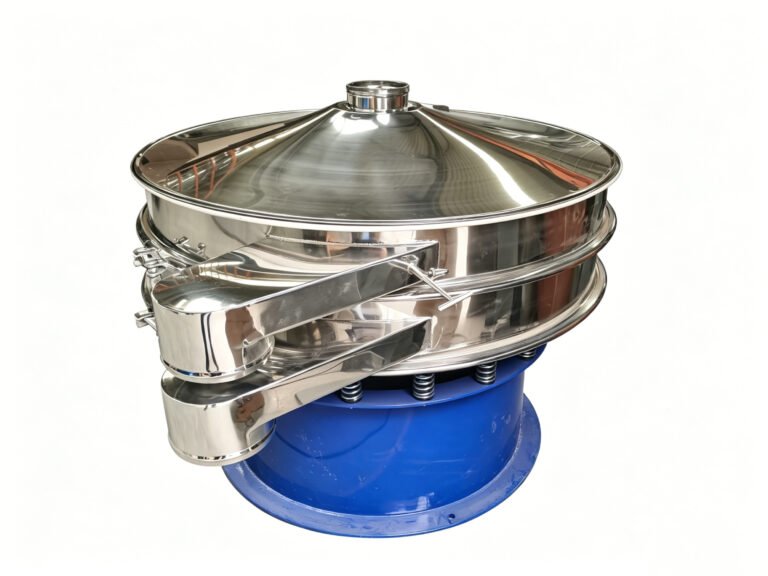
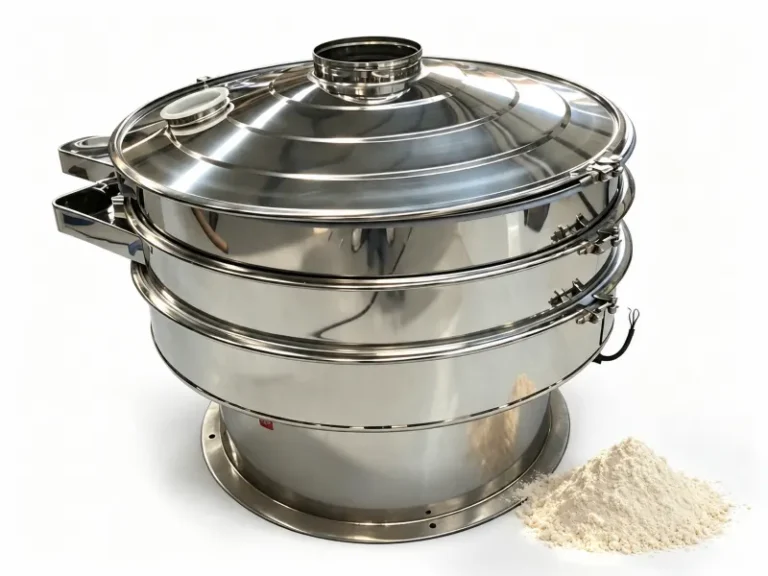
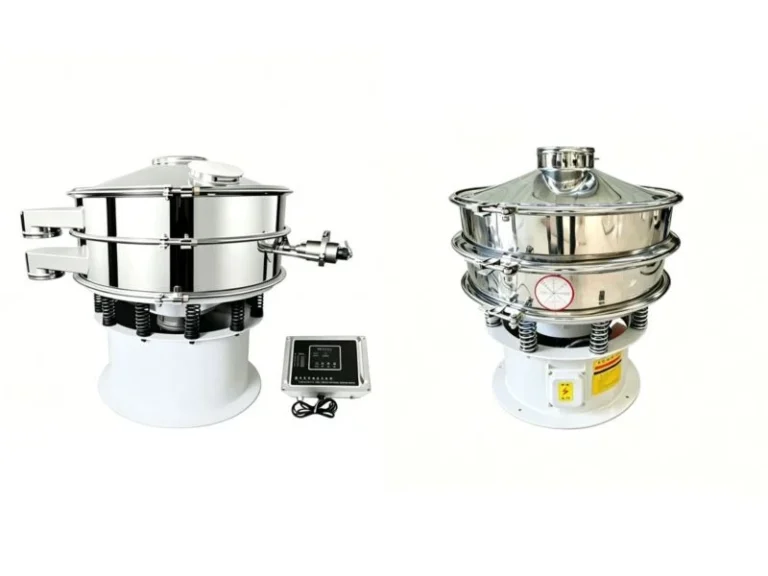
A powder coating vibrating screen removes oversized particles and screen-retained contaminants before packaging or application. To prevent agglomeration and maintain throughput, combine suitable powder storage conditions with uniform feeding, the correct mesh, and ultrasonic de-blinding when conventional screening cannot keep the mesh open.
Powder coatings contain specialized resins, pigments, curing agents, and other additives. Many thermosetting formulations are manufactured by mixing, hot extrusion, cooling, pulverization, and sieving. Fine powders can agglomerate because of moisture, static attraction, heat, or storage pressure. Screening helps control the oversized fraction, but it cannot reverse heat damage or replace proper material handling.
Why Do Powder Coatings Agglomerate
Agglomeration occurs when particles stick together instead of remaining loose and free-flowing. Several conditions can contribute to this problem.
Moisture and Temperature Changes
Moisture can form liquid bridges between particles, while temperature fluctuations may cause condensation. Excessive heat can soften susceptible resin components and encourage caking. These conditions make powder harder to disperse and screen.
Static Electricity
Contact during mixing, conveying, and screening can generate electrostatic charge. Particle attraction can encourage agglomeration and adhesion to the mesh, reducing the open area available for screening.
Storage and Packaging Pressure
Long storage periods, stacked bags, and transport pressure can compact the powder. Soft agglomerates may disperse during screening, but hardened or fused lumps require separate assessment.
Poor Dispersion and Reclaimed Powder
Insufficient dispersion during manufacture can leave unevenly distributed resin, pigment, or additive material. Reclaimed powder may also contain cured particles, fibers, agglomerates, or other contaminants. Contamination and agglomeration are different problems, although both can increase screening rejects.
The main consequences are poorer fluidization and conveying, mesh blinding, reduced throughput, and additional cleaning downtime. Agglomerates also change the apparent particle-size distribution and may cause uneven deposition or visible coating defects. Screening alone cannot guarantee gloss or adhesion, which also depend on formulation, surface preparation, application, and curing.
How a Vibrating Screen Improves Powder Coating Quality
A correctly configured powder sieving machine separates unwanted oversize material while allowing acceptable powder to pass. Its main benefits are cleaner powder, a controlled upper particle-size limit, and more consistent downstream processing.
Removes Agglomerates and Contaminants
Screening can retain hard lumps, oversized metal particles, fibers, and other foreign material according to their size and shape. Some contaminants may still pass through the mesh. Vibration can help disperse loose, soft agglomerates, but the screen is not a grinding machine. Hard or fused lumps should be removed and assessed before reprocessing.
Controls the Oversized Particle Fraction
The selected opening determines which particles can pass. Single-deck safety screening principally removes oversize material; it does not remove all undersize fines or guarantee a narrow particle-size distribution. Mesh examples for virgin powder, reclaimed powder, and finer separation are outlined below.
Supports Grading and Powder Recovery
Where the process requires multiple stages, an initial screen may remove coarse foreign material, a subsequent stage may separate coarse powder for approved regrinding, and further screening may classify acceptable fractions. The sequence should follow the actual production requirements rather than a fixed three-stage layout. Reclaimed powder must still meet the coating supplier’s reuse and quality requirements.
How to Prevent Agglomeration and Mesh Blinding
Preventing new agglomerates and keeping the mesh open require different controls. Storage and temperature management address powder condition, while feeding, mesh selection, and de-blinding address screening performance.
Control Powder Temperature and Humidity
Keep powder dry, avoid condensation, and follow the formulation supplier’s storage and processing instructions. Keep containers closed when not in use and limit exposure to excessive heat during transport.
Reference figures sometimes proposed for process evaluation include 15–30°C and relative humidity below 70% during screening, and below 30°C and below 60% relative humidity during storage. These figures are not universal powder coating limits or verified limits for your formulation. Use them only if confirmed by the powder supplier; some products require cooler or drier conditions. Ambient humidity alone does not establish the powder’s moisture condition.
Use Uniform Feeding
Feed continuously at a controlled rate instead of loading large batches onto one area of the screen. A suitable vibrating feeder can stabilize delivery and maintain an even powder bed. Excessive bed depth limits particle contact with the mesh and can reduce throughput.
Select the Correct Mesh Size
Select the mesh from the required separation size and the powder’s measured particle-size distribution. The following preserves the mesh options considered for this application as trial examples, not universal industry specifications.
| Screening duty | Mesh options to evaluate |
| Virgin powder safety screening | 100 or 120 mesh; 150 or 200 mesh where a finer cut is required |
| Reclaimed powder screening | 60, 80, or 100 mesh, subject to reuse requirements |
| Finer separation trials | 160–230 mesh, including 160–180 and 200–230 mesh options |
| Specialized fine separation | 250 mesh or finer, where the product specification requires it |
These ranges describe different possible duties and should not be combined into one “recommended” mesh range. Confirm the actual opening in microns, wire diameter, and mesh specification with the screen supplier. An unnecessarily fine mesh may reject usable powder, increase blinding, and reduce output.
Optimize Vibration Settings
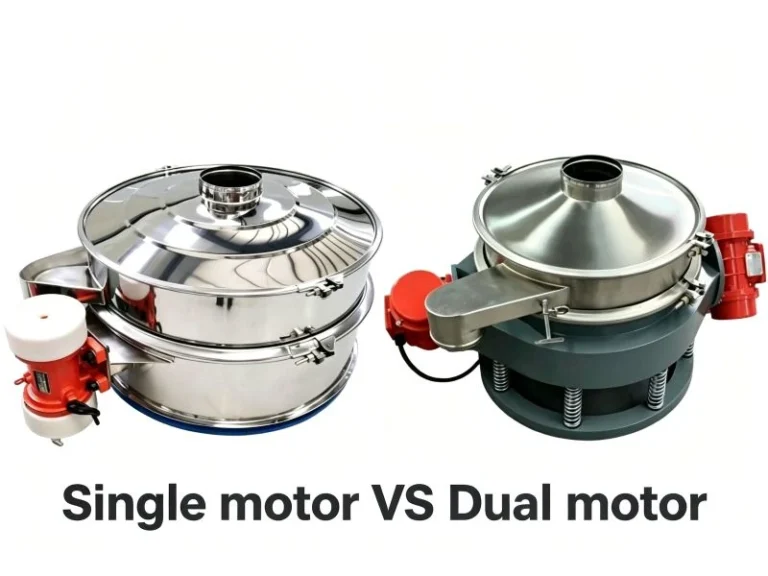
Adjust vibration and material travel so powder spreads evenly and has sufficient opportunity to pass through the mesh. Excessive bouncing can reduce useful screen contact, while inadequate movement can allow buildup. Confirm settings through trials at the intended feed rate, and inspect screen tension, integrity, and cleanliness regularly.
Use an Appropriate De-blinding System
Bouncing-ball cleaning may be considered for compatible, relatively coarse applications, including trials around 100 mesh. Check the cleaning media for wear and contamination risks. For cohesive powders, persistent adhesion, or difficult screening at 200 mesh or finer, ultrasonic assistance may be worth evaluating; mesh count alone does not determine the need.
Un tamis vibrant ultrasonique adds high-frequency vibration directly to the mesh to reduce particle adhesion and keep openings available. The 20–38 kHz range considered here is a reference range, not a setting available on every machine. Yuanjing’s product page describes a broader typical range of 20–40 kHz; confirm the frequency of the supplied generator and transducer. Ultrasonic de-blinding should not be described as electrically neutralizing the powder.
For broader troubleshooting, see our guide to industrial screen clogging causes and prevention.


Conventional or Ultrasonic Screen
A conventional rotary vibrating screen is a practical starting point when the powder flows freely and the mesh remains open. Ultrasonic assistance becomes useful when adhesion and blinding prevent the required output or cause repeated cleaning stops.
| Powder condition | Selection guidance |
| Free-flowing powder without serious clogging | Conventional rotary vibrating screen |
| Raw-material pre-screening or general classification | Conventional screen, subject to the required separation |
| Minor soft agglomerates | Conventional screening may be sufficient; verify reject quality |
| Screening at 200 mesh or finer | Evaluate both performance and blinding; ultrasonic is not automatically required |
| Fine powder with strong adhesion to the mesh | Evaluate ultrasonic de-blinding |
| Frequent blinding, manual cleaning, or falling throughput | Investigate operating conditions and trial ultrasonic assistance |
Compare the two options using the same powder, mesh opening, feed conditions, and acceptance criteria. For a fuller equipment comparison, read ultrasonic vs traditional vibrating screens.
How to Select a Powder Coating Vibrating Screen
Choose the configuration around the material and production requirement, not machine diameter alone.
Powder and separation target: Specify virgin or reclaimed powder, formulation, particle-size distribution, moisture condition, agglomeration severity, and required cut point.
Size and capacity: Yuanjing’s ultrasonic sieve range includes 400–1800 mm diameters. Confirm powder coating throughput in kg/h using trials at the selected mesh and feed conditions rather than treating general catalog capacity as a guarantee.
Construction and cleaning: Options include 304/316 stainless steel and carbon steel. Match contact materials to contamination limits and formulation compatibility, and consider screen access, powder retention, and color-change cleaning.
Installation: Confirm sealing, connections, available space, voltage, and applicable site dust-safety requirements. Avoid treating an enclosed machine as proof that an entire installation meets safety requirements.
Send us your powder type, particle-size distribution, target mesh, required capacity, and current screening problem. Our team can recommend a suitable ultrasonic screening configuration where testing indicates that ultrasonic assistance is needed.