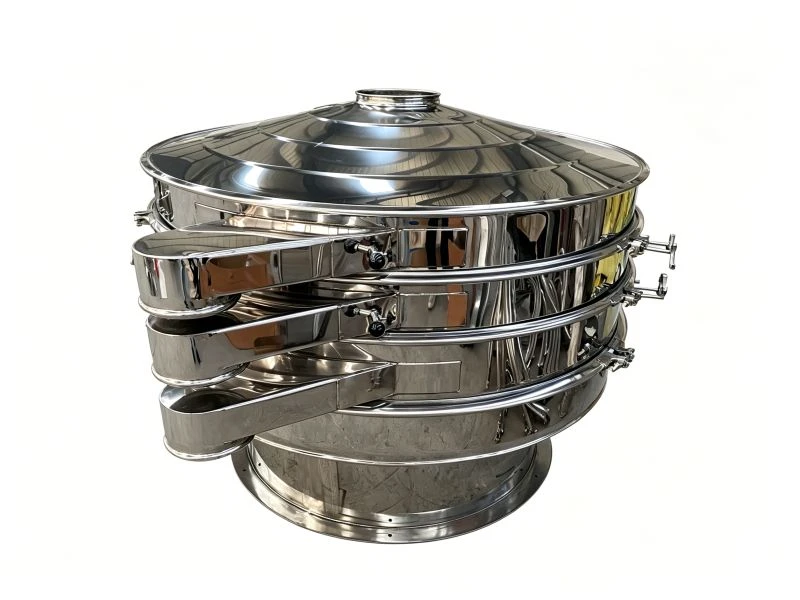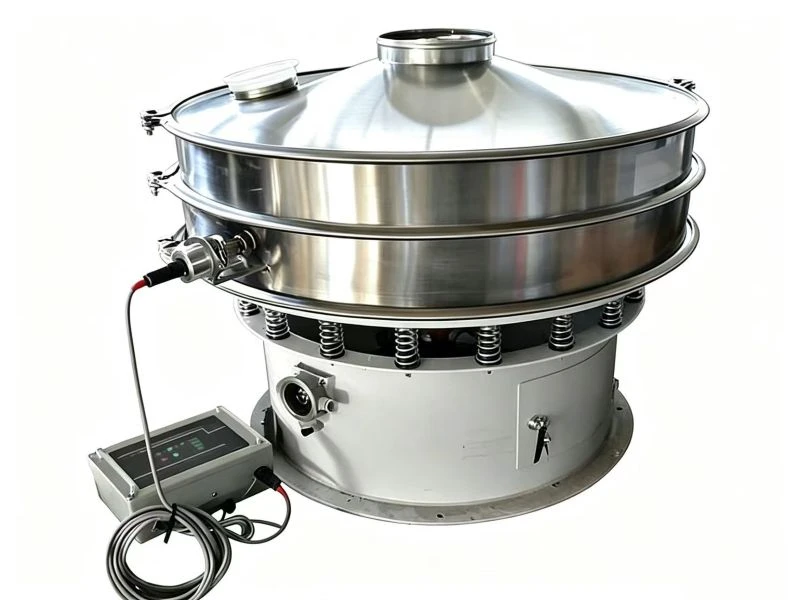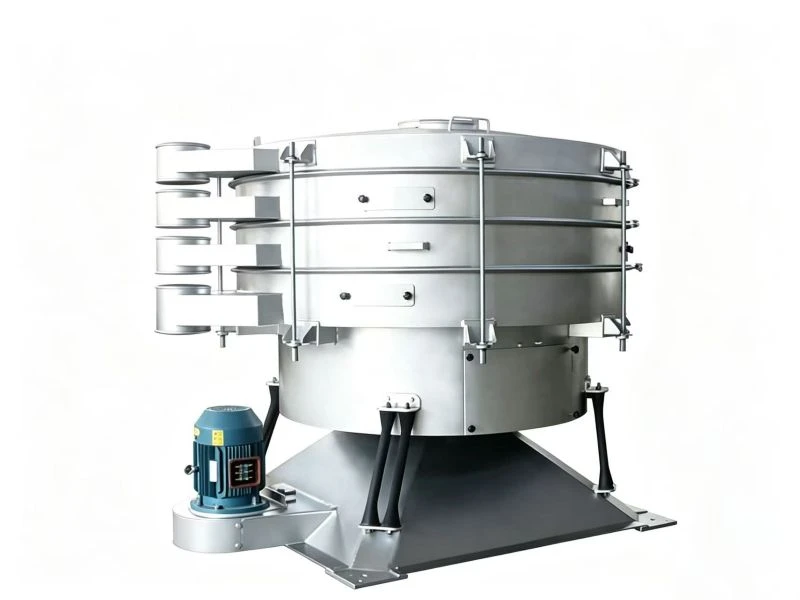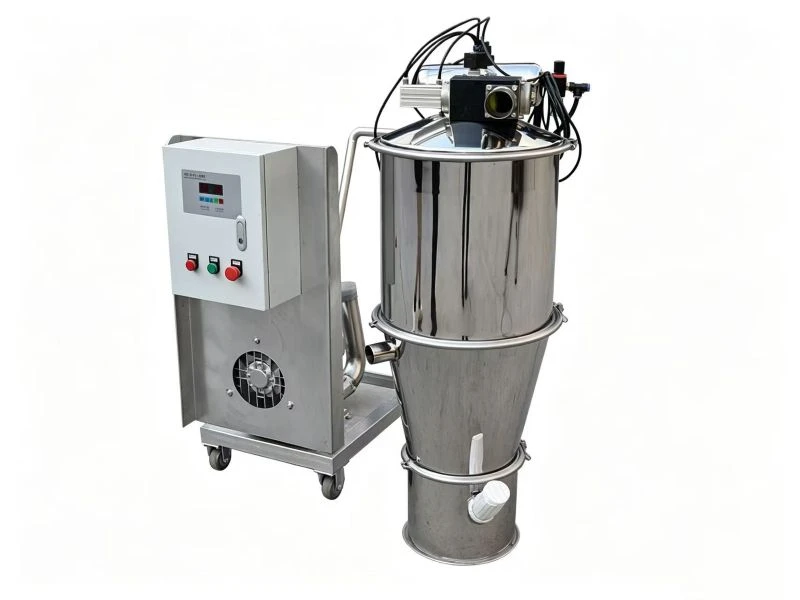

Our screening and conveying equipment is widely used in the chemical industry and is suitable for processing acidic, alkaline, corrosive, and oily chemical raw materials. The equipment is designed to handle powders, granules, and bulk materials safely and efficiently while maintaining stable product quality and high production output.
With durable stainless steel construction, reliable sealing performance, and customizable configurations, our solutions help reduce material contamination, improve screening accuracy, and support continuous operation in demanding chemical processing environments. All systems are designed to meet modern industrial safety and environmental standards.
Application materials
| Powders | Granules | Liquids |
| Calcium Carbonate | Fertilizer Granules | Sulfuric Acid |
| Sodium Carbonate | PVC Resin Pellets | Hydrochloric Acid |
| Titanium Dioxide | Plastic Pellets | Sodium Hydroxide Solution |
| Catalyst Powders | Salt Granules | Acetic Acid |
| Silica Powder | Ammonium Nitrate | Ethylene Glycol |
| Pigments & Dyes | Sugar Granules | Glycerin |
| Polyvinyl Alcohol Powder | Ceramic Beads | Liquid Detergents |
| Soda Ash | Urea Granules | Hydrogen Peroxide |
| Magnesium Oxide Powder | Soda Pellets | Liquid Polymer Resins |
| Talc Powder | Fertilizer Pellets | Industrial Solvents |
Powder coating manufacturers must manage resin, pigment, and additive powders while controlling lumps and contamination. Our guide to powder coating sieving and agglomeration control covers practical screening and equipment selection considerations.
A customer handling non-granulated PTFE composite powder reported caking during transport and even in shallow piles. See our proposed setup for screening non-granulated PTFE composite powder, including the forced mechanism, contact-material considerations, and open-top feeding arrangement.
Processing soda ash, potassium chloride or magnesium sulfate? See our guide to inorganic salt grading and impurity removal for screening applications, deck arrangements and checks for moisture-sensitive materials.
Chemical Industry Standard
Our chemical industry equipment meets global safety, explosion-proof, and corrosion-resistant quality management standards. Parts in contact with chemical materials are made of corrosion-resistant stainless steel or have special coatings, making them suitable for a variety of chemical materials such as acids, alkalis, and solvents, ensuring safe, efficient, and sustainable chemical material handling.
Practical Application
| Material Type | Mesh / Particle Size | Method | Processing Capacity (Kg/h) | Equipment Model |
| Sodium Carbonate | 80 mesh | Dry | 1,200 | Vibro Sifter |
| Calcium Carbonate | 60 mesh | Dry | 1,500 | Rotary Sifter |
| PVC Resin Powder | 100 mesh | Dry | 800 | Tumbler Screen |
| Catalyst Powder | 40–100 μm | Dry | 400 | Linear Vibrating Screen |
| Fertilizer Granules | 2–5 mm | Dry | 2,000 | Screw Conveyor |
| Plastic Pellets | 3–10 mm | Dry | 1,000 | Bulk Handling Conveyor |
| Pigments & Dyes | 60–120 mesh | Dry | 600 | Vibro Sifter |
| Industrial Salt | 2–4 mm | Dry | 1,800 | Pneumatic Conveying System |